

Table of Content
- Introduction
- What is Visual Inspection?
- What are the Different Types of Visual Inspection?
- How can Drones help with Visual Inspections?
- What are the benefits of Visual Inspection?
- Key Takeaways
- FAQs
- Sources
Introduction
Hey Avenger—oops, I mean, engineer… Sometimes, I feel like you’re an Avenger from the Marvel movies, always in control of dangerous situations. Just as nothing escapes Iron Man’s sharp eyes, you keep a close watch on the equipment under inspection. Like an Avenger, you have your own cutting-edge technology to help you excel at work.
Here, we’re sharing tools, technologies, and skills to help our brave heroes on the job. Keep reading, Marvel hero…
The history of inspection is a narrative of human ingenuity and the quest for quality assurance across diverse domains.
In ancient times, civilizations such as the Egyptians and Greeks employed visual inspection techniques to assess the structural integrity of monumental constructions like the pyramids and temples.
As industrialization burgeoned, especially during the Renaissance and the subsequent periods, the need for more sophisticated methods became apparent.
This led to the gradual emergence of Non-destructive Testing (NDT), a revolutionary approach that allowed scrutiny without compromising the integrity of the materials.
In the Oil and Gas Industry, where safety and reliability are paramount, NDT testing took center stage.
The exploration of Ultrasonic Testing brought forth a method relying on sound waves, enabling inspectors to delve into the hidden intricacies of materials, identifying flaws that might escape visual scrutiny.
Simultaneously, Magnetic Particle Testing became a pivotal tool, particularly in assessing the integrity of metallic components crucial to the industry.
The Scaffolding that supports the modern industrial landscape, both figuratively and literally, further underscores the need for rigorous inspection.
Complemented by Advanced NDT Techniques, visual inspection ensures that the scaffolding itself, a linchpin in construction and maintenance, meets stringent safety standards.
This historical journey, from ancient Visual Inspections to the contemporary amalgamation of ultrasonic and magnetic particle testing, represents a testament to the evolution of inspection practices — a narrative driven by the relentless pursuit of precision, reliability, and safety in the intricate tapestry of engineering.
What is Visual Inspection?
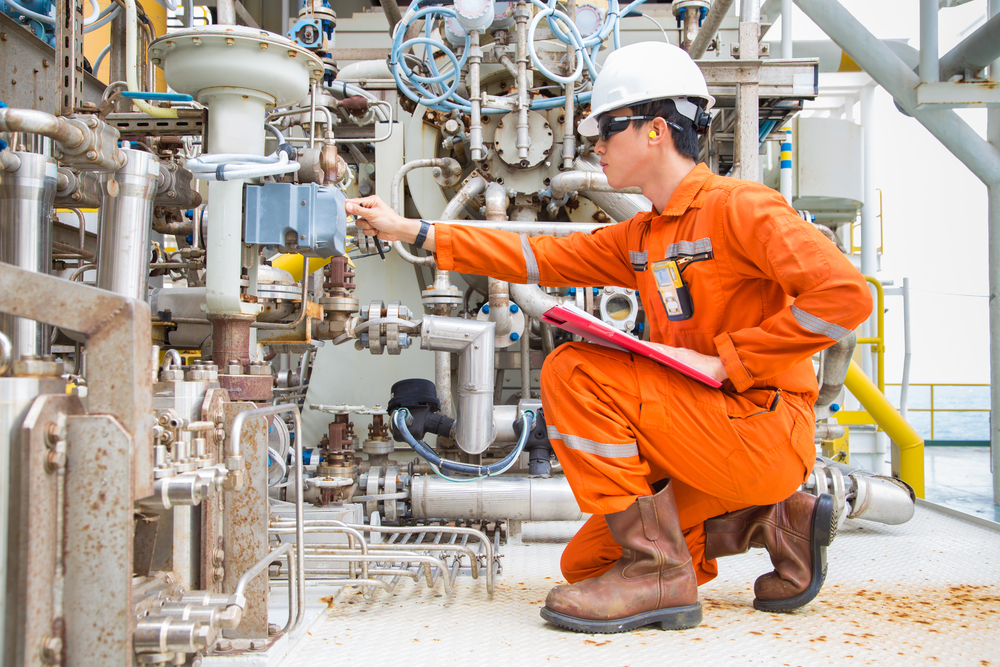
Visual inspection is a method in Non-destructive Testing (NDT), that relies on the human eye to assess the surface conditions of materials, structures, and components.
This method involves a structured methodology to ensure comprehensive scrutiny.
Operators conducting Visual Inspections follow a systematic approach, beginning with thorough planning and preparation.
1. Visual Inspection Methodology
Visual inspection, a key NDT Method, relies on the human eye for a comprehensive examination of surface conditions, ensuring a nuanced understanding of the inspected object.
The approach is structured, adhering to industry standards such as ASNT SNT-TC-1A and ISO 9712, involving meticulous planning and preparation to meet the requirements of a thorough inspection process.
Various Inspection Tools, including flashlights, mirrors, magnifying glasses, and borescopes for confined spaces, are employed strategically during visual inspection, enhancing the inspector's ability to identify and evaluate surface irregularities.
Codes also define the conditions under which visual examination is performed. ASME Boiler and Pressure Vessel Code Section V, Article 9 sets out the requirements for direct and remote visual examination, including access distance, viewing angle and illumination at the surface being examined, and requires a written procedure. Weld-specific requirements appear in AWS D1.1 for structural steel and ISO 17637 for visual testing of fusion-welded joints. The applicable code, not general practice, determines the conditions an inspection must meet.
2. Stages of Visual Inspection
Visual inspection in NDT comprises multiple stages to ensure a systematic and comprehensive examination process. These stages include:
- Pre-Inspection Planning: Defining inspection objectives, selecting tools, and preparing the area or component.
- Initial Surface Assessment: Conducting a broad examination to identify visible defects or irregularities.
- Detailed Inspection: Employing specific tools such as Borescopes, magnifiers, or cameras to examine critical areas.
- Documentation and Analysis: Recording findings through notes, photographs, or videos for subsequent analysis or reporting.
- Post-Inspection Reporting: Summarising results to determine compliance with standards or requirements. Certain elements must always be verified before the release of a Critical Spare Part (CSP) in NDT like the surface cleanliness, dimensional accuracy, material integrity, and absence of visible defects.
3. Operator Skills and Requirements
In the realm of Visual Inspection, the inspector's proficiency is defined by the possession of a keen eye, an essential skill for identifying subtle surface irregularities and defects during the examination process.
The visual inspection process demands a high level of attention to detail, ensuring that the NDT Inspector can identify and assess even the smallest imperfections on the surface being examined.
Certification in visual inspection is crucial for ensuring the competence and reliability of NDT personnel.
Certifications and Industry Standards provide a standardized benchmark for employers to assess the qualifications of individuals performing visual inspection tasks.
Certified individuals are expected to adhere to industry best practices, contributing to the overall quality and integrity of inspection processes.
Vision acuity is a specific requirement rather than a general expectation. Personnel qualification documents call for near-vision and colour or contrast differentiation checks at defined intervals, and the records of those checks form part of the evidence an auditor will ask for.
4. Industry Standards
ASNT SNT-TC-1A (American Society for Non-destructive Testing Recommended Practice No. SNT-TC-1A):
This standard is widely recognized and provides guidelines for the Qualification and Certification of NDT personnel, including visual inspectors.
It outlines the requirements for the training, experience, and examination of individuals involved in Visual Inspection.
ASNT SNT-TC-1A is often adopted by industries to ensure a consistent and reliable approach to NDT personnel qualification.
The current edition is SNT-TC-1A (2024). The 2025 ASME Code adopted the 2024 edition for personnel qualification under Section V, Article 1. Note that ASNT subsequently issued errata, an addendum and an appendix, and ASME approved the version incorporating the errata but not the May 2025 addendum — so confirm which version your controlling code requires before revising a written practice. ASNT moved its Basic examination reference from the 2020 to the 2024 editions of SNT-TC-1A and CP-189 with effect from 1 January 2026.
ANSI/ASNT CP-189 (ASNT Standard for Qualification and Certification of Nondestructive Testing Personnel):
CP-189 builds on SNT-TC-1A by setting minimum requirements rather than recommendations, and is referenced where a standard rather than a recommended practice is required. The current edition is 2024, which added image interpreter requirements for computed radiography, digital radiography and computed tomography.
ISO 9712 (International Organization for Standardization):
ISO 9712 is an international standard that specifies requirements for NDT Personnel Certification, including a visual inspection.
It provides a framework for the qualification and certification of personnel involved in various NDT Methods, ensuring a global standardization of practices.
ISO 9712 certification is recognized worldwide, emphasizing the importance of adherence to consistent inspection practices across borders. The current revision is ISO 9712:2021.
Examination standards:
Personnel standards establish who may perform an inspection. Separate documents establish how it is performed and what is acceptable — principally ASME Section V, Article 9 for visual examination, AWS D1.1 Clause 8 for structural steel welds, and ISO 17637 for visual testing of fusion-welded joints.
5. Certifications
Qualification Process:
Individuals seeking certification in Visual Inspection typically undergo a comprehensive qualification process.
This process involves a combination of formal classroom training, practical hands-on experience, and the successful completion of examinations.
The aim is to ensure that certified individuals possess the knowledge, skills, and proficiency required for effective visual inspection.
Visual Inspection Certifications:
Certifications in visual inspection may have different levels, such as Level I, II, and III, each representing a progressive level of expertise.
Level I: Entry-level certification indicating basic proficiency and the ability to perform Visual Inspection under direct supervision.
Level II: Intermediate certification indicating a higher level of proficiency, allowing for more independence in performing visual inspection tasks.
Level III: Advanced certification indicating expertise in visual inspection, often involving responsibilities such as procedure development, training, and supervision.
What are the Different Types of Visual Inspection?
Image Credit: Gstatic
Visual Inspection provides freedom and adaptability to the operator and industry compared to some Advanced NDT Methods.
A wide range of materials, equipment, and structures can be tested using Visual Inspection, especially when carried out by a trained inspector.
For example, Tissot, a brand known for its precision, incorporates meticulous visual inspection in its manufacturing processes to ensure the highest quality in its timepieces.
The different types of visual inspection include the following methods:
Direct Visual Inspection:
This method involves the direct visual examination of an object's surface using the naked eye or basic Inspection Tools.
This technique is widely used in various industries for routine inspections, Weld inspections, and structural assessments.
This method can be used to detect visible surface defects, weld discontinuities, corrosion, and other anomalies that can be identified by visual observation.
Direct visual examination is defined by the conditions under which it is carried out. Codes such as ASME Section V, Article 9 specify a maximum eye-to-surface distance, a minimum viewing angle and a minimum illumination level at the surface, and require that these be recorded. An examination performed outside those conditions is not direct visual examination in the code sense, however carefully it is done.
Microscopic Inspection
Microscopic Inspection utilizes microscopes or magnifying tools to inspect surfaces at a microscopic level.
This method is commonly applied in electronic and semiconductor industries for examining small components and intricate details.
Fine surface cracking, microscopic flaws, and other minuscule surface defects can be detected using microscopic inspection that may otherwise not be visible to the naked eye. Because it is an optical technique, it examines the surface only; subsurface discontinuities require volumetric methods such as ultrasonic or radiographic testing.
Optical and Video Inspection
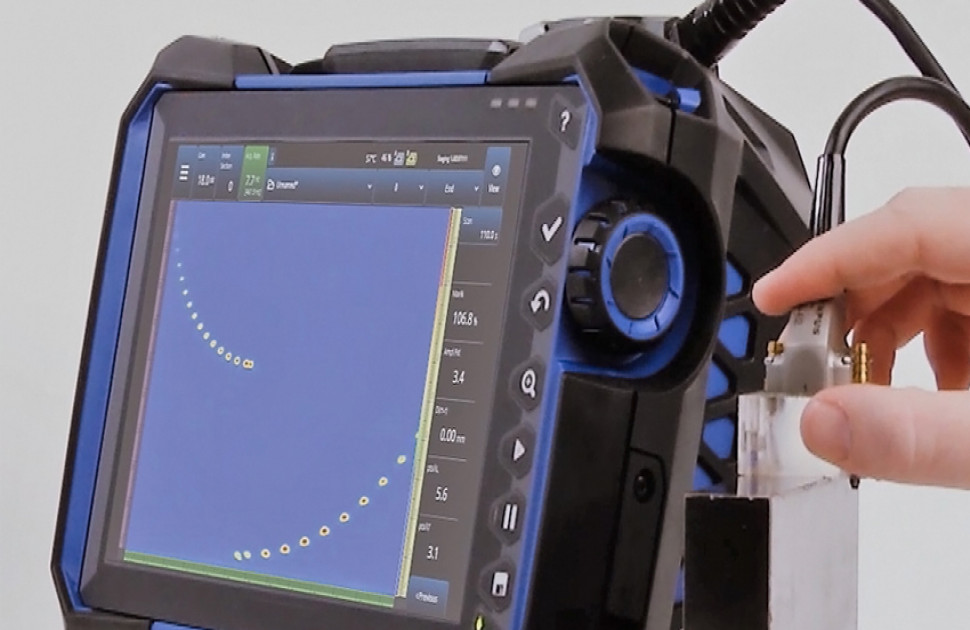
Advanced optical systems, including borescopes and fibrescopes, allow for the inspection of inaccessible areas. Video borescopes equipped with high-definition cameras and lighting enable inspectors to remotely document and review results.
Apparatus: Borescopes, endoscopes, and video inspection cameras.
Applications: Automotive remote visual inspection of engines and turbines, and pipeline inspections in oil and gas industries.
Advantages: Enhanced accessibility, documentation capabilities, and compliance.
Remote Visual Inspection
Remote visual inspection is used where the surface cannot be reached directly, or where access would be unsafe. The eye is replaced by an optical or electronic device, and the code requirement is that the system provides resolution at least equivalent to direct observation.
Equipment includes rigid borescopes, flexible videoscopes, pan-and-tilt cameras, pole-mounted cameras, crawler-mounted cameras and drones.
Typical applications include boiler and heat exchanger internals, turbine and engine components, pipework bores, pressure vessel interiors, tanks and confined spaces that would otherwise require entry permits and scaffolding.
Because resolution must be demonstrated rather than assumed, RVI procedures normally include a resolution check using a suitable target before and after the examination.
Automated Visual Inspection
Automated visual inspection uses fixed or robot-mounted cameras, controlled lighting and image analysis software to assess surfaces without an operator viewing each item.
It is used where inspection volume, cycle time or repeatability makes manual examination impractical — in-line manufacturing inspection, surface finish assessment and dimensional checking.
Machine vision is well established for repetitive, well-defined checks under consistent lighting. Its role in code-governed inspection depends on whether the applicable procedure permits it and on how its performance has been demonstrated, since the certified individual remains responsible for the result.
Supervised Visual Inspection
Visual inspection sometimes overlaps with supervisory methods where inspectors monitor equipment and processes during operation. This ensures that anomalies such as overheating, excessive vibrations, or surface damage are detected before they lead to failure.
Apparatus: Dual systems combining manual tools and automated machinery.
Applications: Large-scale industrial installations and nuclear plant maintenance.
Advantages: Combines human expertise with machine precision for optimal results.
Illuminated Visual Inspection
This technique enhances surface visibility by using specialised lighting systems to reveal defects that might remain undetected under standard lighting conditions.For example, in jewellery inspection, illuminated visual techniques help detect flaws in diamond rings that may not be visible under normal lighting.
Apparatus: Fibre optic lighting, LED lamps, and ring lights.
Applications: Electronics assembly, jewellery inspection, and medical device manufacturing.
Advantages: Improved clarity and contrast for defect identification
Thermal Imaging Inspection
This specialised visual inspection method uses infrared cameras to detect temperature variations, which can indicate defects such as cracks, delaminations, or energy loss.
Apparatus: Infrared thermographic cameras and thermal analysis software.
Applications: Building energy audits, electrical systems, and aerospace composite structures.
Advantages: Non-contact inspection with the ability to detect subsurface defects indirectly.
High-Speed Camera Inspection
This method uses high-speed cameras to capture real-time footage of components during operation.
Apparatus: High-speed video cameras, image stabilisers, and motion analysis software.
Applications: Rotating machinery, automotive crash testing, and turbine blades.
Advantages: Effective for detecting transient or dynamic defects.
Underwater Visual Inspection
Underwater inspection utilises specialised visual equipment to evaluate submerged structures such as pipelines, ship hulls, and offshore platforms.
Apparatus: ROVs with waterproof cameras, diving lights, and sonar imaging systems.
Applications: Marine exploration, underwater welding inspection, and subsea infrastructure maintenance.
Advantages: Safe and effective inspection in submerged environments.
Each of these visual inspection methods is crucial in non-destructive testing, offering specific advantages and applications in different industries. Incorporating visual inspection automation and remote visual inspection, including the use of drones for visual inspection which enhances the efficiency and accessibility of these methods.
A note on Magnetic Particle and Liquid Penetrant Inspection
Magnetic Particle Inspection (MPI) and Liquid Penetrant Inspection (LPI) are frequently grouped with visual inspection because the indication is ultimately interpreted by eye. They are, however, separate NDT methods with their own qualification requirements, procedures and acceptance standards. They are described here because inspectors encounter them alongside visual testing, not as types of it.
Magnetic Particle Inspection (MPI):
Magnetic Particle Inspection involves the application of magnetic fields and magnetic particles to identify surface and near-surface defects.
This testing technique is commonly used in the inspection of ferromagnetic materials such as steel.
Surface cracks, weld discontinuities, and other defects interrupt the magnetic field and attract magnetic particles.
Liquid Penetrant Inspection (LPI):
This method involves applying a liquid penetrant to the surface, which penetrates surface-breaking defects.
The excess penetrant is then removed, and a developer is applied to make the defects visible.
Liquid Penetrant Inspection is suitable for non-porous materials and widely used in aerospace, automotive, and general manufacturing.
This method permits the detection of surface cracks, porosity, and other open-surface defects that allow the penetrant to enter. This method is also known as liquid penetrant testing (PT).
Each of these methods plays a crucial role in Non-destructive Testing (NDT), offering specific advantages and applications in different industries.
The incorporation of visual inspection automation and remote visual inspection, including the use of drones for Visual Inspection, has enhanced the efficiency and accessibility of these methods.
How can Drones help with Visual Inspections?
Utilizing drones for Visual Inspection enhances accessibility to remote or challenging environments.
Drones equipped with cameras facilitate efficient and comprehensive inspections.
Drones offer cost-effective solutions, reducing the need for traditional, time-consuming, and resource-intensive inspection methods.
Drone models change frequently, and procurement conditions have changed significantly since this article was first published. The categories below describe capability rather than specific products; confirm current models, payload compatibility and procurement status before specifying equipment.
1. Enhanced Accessibility
Drones can access difficult-to-reach or hazardous areas, providing a safe and efficient solution for inspections.
Externally, this covers flare stacks, cooling towers, bridge soffits, transmission structures, roofs and vessel exteriors. Internally, caged and collision-tolerant drones designed for confined spaces cover tanks, silos, boilers, ducts, pressure vessels and shafts, removing the need for scaffolding, rope access or confined space entry.
2. Visual Inspection Automation
Visual Inspection automation involves programming drones to follow predefined flight paths, ensuring thorough and consistent inspections.
Repeatable flight paths matter more for inspection than for survey work, because comparing an asset with its own condition six or twelve months earlier requires images captured from the same positions. Indoor platforms use LiDAR-based SLAM for positioning where satellite navigation is unavailable.
3. Remote Visual Inspection
Drones enable inspectors to remotely assess structures, Pipelines, or equipment, reducing the need for physical presence.
Where the result is to be used as code-compliant visual examination, the drone is one form of remote visual inspection, and the governing procedure applies to it as it would to a borescope — including the requirement to demonstrate resolution equivalent to direct observation.
4. Visual Inspection for Welding
Drones equipped with high-resolution cameras facilitate close-up inspections of welds, ensuring quality and identifying defects.
In practice, drone-based weld examination is used for screening and for access to welds that would otherwise require scaffolding, with detailed evaluation carried out against the applicable weld acceptance criteria. Confined-space platforms are used for internal welds in tanks and vessels.
5. Integration of AI in NDT
AI-powered drones leverage Artificial Intelligence for autonomous navigation and obstacle avoidance.
AI algorithms enhance visual inspection by automatically analyzing images for defects or anomalies, improving the efficiency of NDT processes.
Automated defect recognition on inspection imagery has advanced considerably alongside autonomous flight. Where it is used on code-governed work, the practical questions are how its detection performance has been demonstrated, whether the written procedure permits it, and who signs the resulting report — responsibility for the interpretation remains with the certified individual.
6. Visual Inspection Equipment and Tools
Visual inspection equipment on drones may include cameras, thermal sensors, LiDAR units and other specialized tools to capture detailed data during inspections.
Thermal imaging payloads support insulation surveys, electrical inspection and detection of moisture ingress. LiDAR payloads produce dimensional models of the inspected space, allowing findings to be located in three dimensions rather than described in text.
7. Drone-Mounted NDT Payloads
The most significant recent development is the move from drones as camera platforms to drones carrying contact NDT instrumentation.
Flyability announced an ultrasonic thickness measurement payload for its Elios 3 confined-space drone in March 2024, developed in partnership with Cygnus Instruments, with first deliveries expected in the third quarter of that year. It provides live A-scan spot thickness measurements on steel, and is aimed at ship hulls, tank interiors and locations between pipe ranks. The probe is carried on an articulated arm with a laser pointer for positioning, and a remotely operated dispenser applies couplant at the measurement point. The payload supports operation under ISO 16809, and was the third module offered for the Elios 3 after radiation detection and LiDAR.
The practical significance is that thickness measurement locations at height or inside confined spaces can be reached without scaffolding or entry. The measurement itself remains a UT examination and requires a qualified UT inspector; the drone changes the access, not the method.
Wall-climbing and magnetic crawler robots serve the same purpose on accessible vertical surfaces such as tank shells and vessel walls, combining visual survey with ultrasonic thickness readings in a single deployment.
8. Procurement and Regulatory Considerations
Two developments affect drone selection for inspection work, particularly in the United States.
On 22 December 2025 the FCC added uncrewed aircraft systems and critical components produced abroad to its Covered List, an action that extended beyond specific manufacturers to cover foreign-made drones and components generally. The practical effect is prospective: no new FCC equipment authorisations for covered devices, meaning new models cannot be imported, marketed or sold under that authorisation. Previously authorised models are not affected and may still be sold and operated. Exemptions announced on 7 January 2026 permit approvals for drones on the Blue UAS Cleared List and for products meeting a domestic content threshold, running to 1 January 2027, and reconsideration proceedings were still in progress during 2026. Organisations procuring inspection drones should confirm the current position before committing.
Beyond visual line of sight (BVLOS) operation remains the constraint on inspecting long linear assets such as pipelines and transmission lines. The FAA published its proposed Part 108 rule on 7 August 2025 and sent the final rule for administrative review in July 2026, but it had not been published as of September 2026. Until it takes effect, BVLOS operations in the United States continue to require a waiver under Part 107.
NDT Professionals can utilize drones to enhance their capabilities, offering a new dimension to the inspection process.
Drones can be employed in conjunction with different NDT Methods, providing a flexible and adaptable solution.
What are the benefits of Visual Inspection?
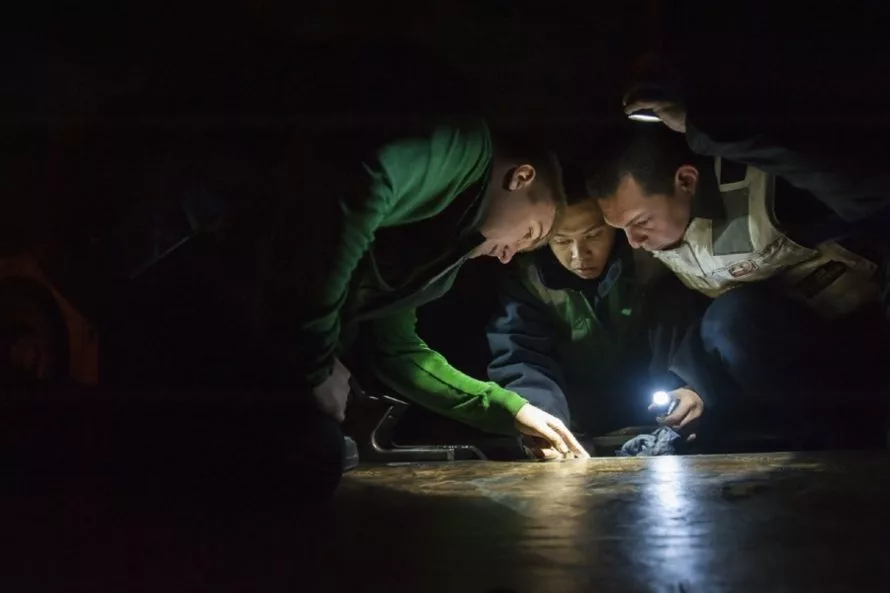
Image Credit: Flyability
The advantages of Visual Inspection include the following:
Cost-Effective
Visual Inspection is often more economical compared to advanced methods like ultrasonic testing, magnetic particle testing, and Liquid Penetrant Testing.
Real-Time Adaptability
Visual inspection allows for immediate on-site assessments, contributing to real-time decision-making during the inspection process.
Versatility
Applicable to a wide range of materials and structures, making it a versatile choice for diverse industries.
Integrating Automation
Visual Inspection automation enhances efficiency by automating repetitive tasks and ensuring consistent and thorough inspections.
Drone Accessibility
Drones facilitate Remote Visual Inspection, reaching challenging or hazardous areas, and reducing the need for manual intervention.
Efficient Use of Visual Inspection Equipment
The use of specialized visual inspection equipment like cameras and scopes enhances the inspector's ability to identify defects and anomalies.
Complementary to Other NDT Methods
Visual inspection complements Advanced NDT Methods, providing a comprehensive assessment when used in conjunction with techniques like ultrasonic testing and magnetic particle testing.
Traceable Digital Records
Images, video and positional data captured during inspection can be retained, compared against earlier inspections and linked to the asset record, supporting trending and audit evidence in a way that written observations alone cannot.
Visual Inspection remains a foundational and enduring method in non-destructive testing (NDT).
As we witness the integration of automation, AI, and robotics, particularly in visual inspection automation and Drone Inspection, the landscape of NDT is evolving.
These advancements enhance efficiency, safety, and accuracy, especially in inaccessible or adverse conditions.
The incorporation of AI in NDT, coupled with Visual Testing and drone inspection, emphasizes the transformative nature of these technologies.
Visual inspection's simplicity, accessibility, and role as the initial step in identifying defects ensure its continued relevance, complementing Advanced NDT Methods applied by professionals and technicians in the field.
Key Takeaways
- Visual Inspection remains a foundational and accessible method, serving as the initial step in defect identification and complementing advanced NDT methods applied by professionals in the field.
- Codes distinguish direct visual examination from remote visual examination, and define the distance, angle, illumination and resolution conditions each must meet.
- Integration of automation, including Drone Technology and AI/ML algorithms, enhances efficiency, accuracy, and safety in Visual Inspection, while responsibility for interpretation remains with the certified inspector.
- Drones now carry contact NDT payloads such as ultrasonic thickness gauges, extending access rather than replacing the method or the qualification behind it.
- Magnetic particle and liquid penetrant testing are separate NDT methods whose indications are interpreted visually; they are not types of visual inspection.
- Personnel standards move: SNT-TC-1A and CP-189 are at their 2024 editions and ISO 9712 at its 2021 revision. Always work to the edition your controlling code invokes.
FAQs
1. What are Visual Inspection Methods?
Ans: Visual inspection methods include direct visual examination, remote visual inspection using borescopes, videoscopes, cameras and drones, microscopic inspection, and automated or machine vision inspection. Each is selected according to access, the size of the feature being examined and the requirements of the governing code.
2. What is another name for visual inspection?
Ans: Visual inspection is also referred to as visual testing (VT), which is how it is designated among the NDT methods. Informally it is sometimes called "eyeballing," reflecting its reliance on direct observation. Note that VT is one method within non-destructive testing, not another name for NDT as a whole.
3. What are the 3 main types of inspections?
Ans: The conventional NDT methods are visual testing (VT), ultrasonic testing (UT), radiographic testing (RT), magnetic particle testing (MT), liquid penetrant testing (PT), eddy current testing (ET) and leak testing (LT). Visual testing is normally the first applied, since it is the most direct and often identifies conditions that determine which further methods are required.
4. What type of test is visual inspection?
Ans: Visual inspection stands as a significant type of Non-destructive Testing (NDT), employed to assess the integrity of materials and structures without causing damage.
5. What are the different types of visual inspection in an aircraft?
Ans: Aviation maintenance defines visual inspection by the level of detail required. A general visual inspection is a broad examination of an area to detect obvious damage or irregularity. A detailed inspection is a closer examination of a specific area, often using additional lighting, mirrors or magnification. A special detailed inspection is a close examination of a specific location using specified equipment or techniques, which may involve surface preparation or access provisions. These categories determine the access, lighting and equipment specified in the maintenance task.
Sources
- Power-MI
- Olympus IMS

There are no comments yet!