

Table Of Content
- What is Ultrasonic Testing?
- What is an Ultrasonic Testing Procedure?
- Important Terms in Ultrasonic Testing
- Ultrasonic Testing Techniques and When They Apply
- Basic Requirements for Ultrasonic Testing
- Need for Ultrasonic Testing Procedure
- Formulating a Procedure for Ultrasonic Testing
- Requirements of an Ultrasonic Examination Procedure
- Surface Preparation in Ultrasonic Testing NDT Procedures
- Equipment required for Ultrasonic Testing Procedures
- Calibration and Reference Standards
- Step-by-Step Ultrasonic Testing Procedure
- Ultrasonic Testing Procedures - An Enabler of Longevity
- Key Takeaways
- FAQs
What is Ultrasonic Testing?
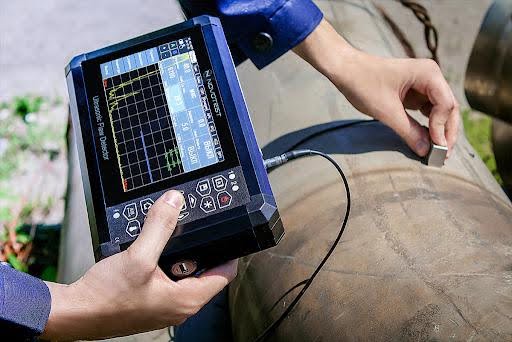
Ultrasonic testing is a versatile and indispensable method in NDT, capable of detecting a broad spectrum of discontinuities including cracks, voids, laminations and inclusions, while being non-invasive and highly accurate.
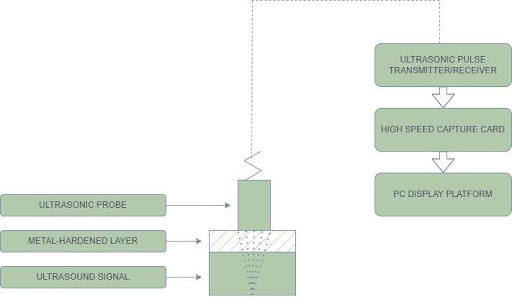
Ultrasonic testing detects internal discontinuities using high-frequency sound waves above the range of human hearing. It works on materials that transmit sound adequately, which covers most metals and many other engineering materials.
Its limits are worth stating at the outset. Materials with high sound attenuation — coarse-grained castings, austenitic stainless steel welds with their directional grain structure, and porous composites — scatter and absorb the beam, which reduces signal clarity and can make the method unsuitable without specialised probes or techniques. Discontinuities oriented parallel to the beam may also go undetected, because they reflect little energy back toward the probe.
What is an Ultrasonic Testing Procedure?
The procedure for ultrasonic testing entails the generation of high-frequency sound waves by a transducer, which are directed into the material under examination.
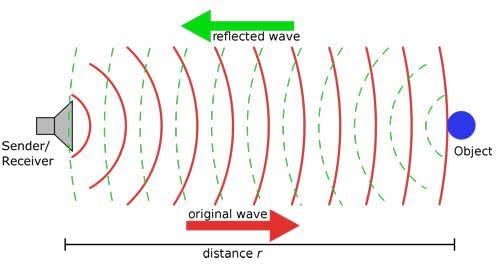
As these sound waves propagate through the material, they encounter boundaries between different media or internal discontinuities, and reflect back toward the transducer.
Qualified technicians analyse the time taken for the sound waves to return and their amplitude, allowing the location and size of discontinuities within the material to be determined, and their nature to be assessed against known signal characteristics.
A written procedure is the controlled document that defines how all of this is done on a given job — which technique, which probe, which frequency, how the system is calibrated, how indications are evaluated, and against which acceptance criteria.
Important Terms in Ultrasonic Testing
Some important terms in ultrasonic testing that are vital to understanding UT procedures include:
Transducer:
The transducer emits ultrasonic waves and receives echoes. It is a pivotal component of ultrasonic testing equipment.
Couplant:
A coupling medium, typically a gel or liquid, applied between the transducer and the test surface to exclude air and allow sound to pass into the material.
Echo:
When an ultrasonic wave encounters a boundary or discontinuity within the material, it reflects back to the transducer, creating an echo. The time of flight and amplitude of these echoes are used to assess the material's condition.
Wavelength:
Wavelength is the distance over which the wave repeats — the distance between two successive corresponding points, such as two adjacent compressions. It is inversely proportional to frequency, so higher-frequency waves have shorter wavelengths. Wavelength matters practically because it sets a limit on the smallest reflector a given setup can resolve.
Frequency:
Ultrasonic waves are generated at specific frequencies. The choice of frequency depends on the material, its thickness and the nature of the discontinuity being sought. Higher frequencies give better resolution and sensitivity to small reflectors but penetrate less; lower frequencies penetrate further through thick or attenuative material at the cost of resolution.
Velocity:
Velocity refers to the speed at which ultrasonic waves travel through a material. It is a critical parameter in calculating thickness and in locating discontinuities, and it differs between materials and between wave modes — longitudinal waves travel faster than shear waves in the same material.
Attenuation:
The progressive loss of sound energy as the beam travels through material, caused by absorption and by scattering at grain boundaries. Attenuation increases with frequency and with grain size, and is the main reason some materials are difficult to inspect.
Ultrasonic testing is a crucial NDT method for inspecting materials and structures. Proper equipment, adherence to standardised procedures, and command of the key terminology are essential for achieving accurate and reliable results.
Ultrasonic Testing Techniques and When They Apply
A procedure has to specify which technique is used, because the technique determines what the inspection can find. The main options are:
Straight beam (normal incidence):
A longitudinal wave is introduced perpendicular to the surface. Used for thickness measurement, and for detecting laminations, inclusions and discontinuities oriented parallel to the surface. It is the standard technique for plate, forgings and corrosion mapping.
Angle beam:
A wedge introduces a shear wave at an angle, commonly 45, 60 or 70 degrees. This is the standard technique for weld examination, because most weld discontinuities — lack of fusion, incomplete penetration, cracks in the fusion face — are oriented such that a normal beam would miss them.
Pulse-echo and through-transmission:
In pulse-echo, one transducer both transmits and receives, and the discontinuity is located from the time of flight. In through-transmission, separate transmitting and receiving probes sit on opposite faces, and a discontinuity is indicated by loss of transmitted signal. Pulse-echo gives depth information; through-transmission does not, but tolerates higher attenuation.
Time-of-flight diffraction (TOFD):
Uses diffracted signals from the tips of a discontinuity rather than reflected amplitude, which makes it effective for through-wall height sizing and relatively insensitive to flaw orientation. Commonly applied to weld examination alongside pulse-echo.
Phased array ultrasonic testing (PAUT):
A multi-element probe steers and focuses the beam electronically, sweeping through a range of angles from a single position. It improves coverage on complex geometry and produces sectorial images that support both detection and sizing. PAUT and TOFD are frequently specified together for weld inspection, and encoded scanning allows the result to be recorded and re-examined.
Corrosion mapping:
Encoded straight-beam scanning that produces a thickness map of an area rather than discrete readings, used for wall loss assessment on vessels and pipework.
Selection is driven by the material, geometry, expected discontinuity type and orientation, and by what the governing code permits. Encoded techniques such as PAUT, TOFD and corrosion mapping also produce a permanent record, which matters where inspections will be compared over time.
Basic Requirements for Ultrasonic Testing
The basic requirements for performing ultrasonic inspections include:
Ultrasonic Testing Equipment:
Essential equipment includes an ultrasonic flaw detector, transducers (or probes) with the necessary wedges, and a couplant.
The flaw detector generates the excitation pulse and processes the received signals; the transducers convert electrical energy into sound and back again; the couplant allows the sound to pass into the part.
Calibration Standards:
Calibration and reference blocks contain artificial reflectors of precisely known size and position — side-drilled holes, flat-bottom holes and machined notches — which serve as the reference against which instrument settings and system performance are established. The block material should represent the acoustic properties of the component being inspected.
Surface Preparation:
Thorough surface preparation is vital to ensure accurate results. The material's surface should be clean and free from contaminants that could hinder sound transmission.
Training and Certification:
Properly qualified personnel are essential. Technicians are qualified and certified under a recognised scheme — an employer's written practice based on ASNT SNT-TC-1A (currently at its 2024 edition) or ANSI/ASNT CP-189, or third-party certification under ISO 9712:2021. The level of certification determines what an individual may do: Level I typically performs set-ups and acquires data under supervision, Level II interprets and evaluates against the acceptance criteria, and Level III has responsibility for procedures, techniques and qualification.
Need for Ultrasonic Testing Procedures
Efficient industrial operations require a standard operating procedure. For special processes such as non-destructive testing, approved written procedures are essential, and they are normally derived from the governing code or standard.
A few of the global inspection standards for ultrasonic testing include:
- ASME Boiler & Pressure Vessel Code, Section V — Article 4 for ultrasonic examination of welds, Article 5 for ultrasonic examination methods for materials and fabrication, with Article 23 adopting the relevant ASTM standards
- BS EN ISO 17640 — ultrasonic testing of welded joints, with ISO 11666 for acceptance levels and ISO 23279 for characterisation of indications
- AWS D1.1, Clause 8 — ultrasonic testing of structural steel welds
- ASTM E164 (contact examination of weldments), ASTM E114 (pulse-echo straight beam contact examination), ASTM E317 (evaluating performance characteristics of ultrasonic systems) and ASTM E797 (thickness measurement by manual contact)
- SAE AMS 2630 and SAE AMS 2632 — aerospace standards
Note the distinction between the standard that says how to examine and the standard that says what is acceptable. ISO 17640 describes the technique; ISO 11666 gives the acceptance levels. The procedure must reference both, and acceptance criteria are ultimately set by the construction code, the specification or the contract.
A well-defined procedure in ultrasonic testing provides significant benefits, including:
Consistency:
Procedures ensure consistent testing, minimising human error and reducing variability in results.
Safety:
Proper procedures incorporate safety guidance covering the work environment — hot surfaces, working at height, confined space entry — and the selection of couplants, since halogen and sulphur content is restricted on stainless steels and nickel alloys, and couplant must be removed after inspection.
Standardisation:
Following established procedures helps maintain uniformity and compliance with industry standards and regulations.
Quality Assurance:
Procedures enable the accurate detection and documentation of discontinuities, supporting the quality and reliability of materials and structures.
Training:
Procedures are valuable training tools for technicians, guiding them in understanding and implementing best practices.
Formulating a Procedure for Ultrasonic Testing
A well-defined ultrasonic testing procedure must include the following:
1. Scope: This section delineates the range of the procedure, specifying the materials, thickness range, types of weld joint, and techniques covered.
2. References: It includes citations of the international or local standards the procedure adheres to, with their editions.
3. General Requirements: This part outlines the fundamental prerequisites, including:
- Personnel qualifications
- Equipment capability requirements
- Search unit size, frequency and angle (probe)
- Couplant specification, including any restrictions on halogen and sulphur content
- Calibration and reference standards
- Surface condition and preparation requirements
4. Inspection Procedure: Here, the step-by-step process of conducting the inspection is detailed, including calibration, scanning pattern, scan overlap, scanning speed, scanning sensitivity and the extent of coverage.
5. Evaluation of Indications: This section covers how indications detected during the inspection are assessed — the recording level, how geometric indications are distinguished from relevant ones, and how length and through-wall height are determined.
6. Acceptance Criteria: It sets forth the criteria for determining whether the inspected material meets the required standards, referenced to the governing code or specification rather than stated in isolation.
7. Documentation & Report Format: This component outlines the format and content requirements for documenting inspection results, including the instrument and probe identification, calibration block used, calibration times, technique details, and the qualification of the person performing and evaluating the examination.
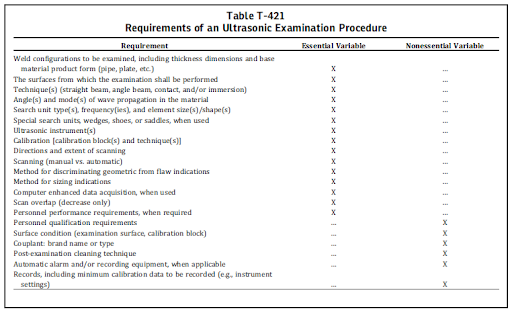
The procedure should encompass all essential variables mentioned in relevant standards, such as those outlined in ASME Section V Article 4.
Requirements of an Ultrasonic Examination Procedure
The procedure must address all the essential variables identified in the governing standard — for example, the table of essential and non-essential variables in ASME Section V, Article 4.
The distinction matters in practice. Under ASME Section V, Article 4, essential variables include the search unit type, frequency and element size; the beam angle and wave mode; the examination technique; the calibration method; and the direction and extent of scanning. Where the referencing code requires procedure qualification, changing any of these requires the procedure to be requalified by demonstration. Non-essential variables — such as couplant brand or type, surface condition and post-examination cleaning — can be changed by revising the procedure, without requalification. Knowing which is which is what prevents a routine substitution from invalidating the examination.
Where the code requires it, the procedure is qualified by demonstration on a representative test piece, and the demonstration record is retained as part of the quality documentation.
Surface Preparation in Ultrasonic Testing Procedures
Effective surface preparation is a fundamental aspect of ultrasonic testing, ensuring reliable results. Key factors include:
Clean Surface for NDT:
A clean surface is essential for accurate results. The test subject should be free from contaminants such as dirt, oil, loose scale, rust and, where required, paint.
These substances interfere with the transmission and reception of ultrasonic waves, affecting the reliability of the examination. Note that a well-bonded coating of known thickness can sometimes be left in place if the procedure allows for it, but loose or uneven coating cannot.
Surface Smoothness in Ultrasonic Examination:
The surface should be smooth and free of rough or irregular areas that could scatter the beam or prevent consistent coupling.
This becomes particularly critical when inspecting materials with complex geometries, where probe contact is already difficult to maintain.
Optimal Couplant Application:
Couplant, a specialised gel or liquid, is applied between the transducer and the surface to exclude air and allow sound to enter the material.
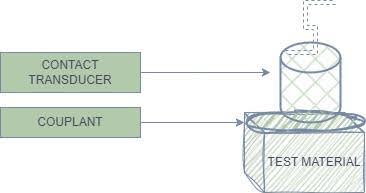
The same couplant should be used for calibration and for inspection, since a change in couplant alters the transmitted energy and therefore the reference level. Consistent application matters as much as the choice — variation in couplant thickness changes the transmitted energy and therefore the signal amplitude.
Addressing Surface Irregularities:
Surface irregularities such as pitting or corrosion should be assessed individually, as they affect both coupling and the interpretation of results.
Where the scanning surface is irregular, reference blocks with representative surface condition help establish the transfer correction needed so that amplitudes measured on the component can be compared with those from the calibration block.
Equipment Required for Ultrasonic Testing Procedures
Search Units in Ultrasonic Testing Inspection:
Search units, commonly referred to as transducers or probes, are the heart of the ultrasonic system. They emit ultrasonic waves into the material and receive the returning echoes.
They come in various types, differing in frequency, element size, damping and configuration — single element, dual element for corrosion and thin sections, angle beam with wedges, and array probes — each suited to particular applications.
Screen Height Linearity in NDT Ultrasonic Testing:
Screen height linearity is a verification of the instrument's amplitude response: it confirms that the height of the displayed signal is proportional to the amplitude of the signal received, across the usable screen range.
It matters because evaluation of indications is based on comparing echo amplitude against a reference level. If the display response is not linear, that comparison is unreliable. Screen height linearity is checked at defined intervals under standards such as ASTM E317 and the ASME Section V requirements, and the check is recorded.
Note that depth and distance accuracy are a separate matter, established by calibrating the horizontal sweep against known reflectors and by using the correct material velocity.
Amplitude Control in NDT Testing:
Linguistics of amplitude control refers to the precise adjustment of ultrasonic signal strength and echoes during NDT testing.
This control is a vital consideration, as it allows for detecting subtle indications by amplifying or reducing signal amplitudes.
It is especially pertinent when working with various materials and flaw sizes in NDT ultrasonic testing techniques.
Couplant Use in Ultrasonic NDT Testing:
Couplant ensures proper acoustic contact between the transducer and the material.
Selection depends on the application, the surface temperature and the material under inspection. Typical choices include gels, oils, pastes and water-based solutions, with high-temperature couplants available for hot surfaces. Halogen and sulphur content must be controlled for austenitic stainless steels and nickel alloys, and residues should be removed after the examination.
Read Now - A Comprehensive Guide on Ultrasonic Testing Equipments
Calibration and Reference Standards
Calibration is where most of the reliability of an ultrasonic examination is decided, and it is the part most often compressed in general descriptions of the method.
Calibration blocks:
Standard blocks such as the IIW V1 and V2 are used to establish probe index point, beam angle, sweep range and resolution. Step wedges and thickness standards are used for thickness applications. Basic calibration blocks for weld examination carry side-drilled holes or notches at defined depths in material representative of the component, so that the response from a known reflector can be established at the relevant sound path distances.
Sweep range calibration:
The horizontal axis is calibrated so that displayed distance corresponds correctly to sound path or depth, using known reflectors and the correct material velocity.
Distance amplitude correction (DAC) and time corrected gain (TCG):
Echo amplitude from an identical reflector falls with distance, because of beam spread and attenuation. A DAC curve plots the response from the same reflector at increasing sound paths so that indications can be evaluated against a distance-compensated reference. TCG achieves the same by increasing gain with time so that equal reflectors give equal screen heights, which is the more common approach in encoded and phased array work.
Reference sensitivity and transfer correction:
Scanning sensitivity is set relative to the reference level established on the calibration block. Where the component's surface condition or attenuation differs from the block, a transfer correction is determined and applied.
Calibration checks:
Calibration is verified at the intervals required by the procedure — typically at the start of work, at defined time intervals, on any change of probe, cable or operator, and at the end of the examination. If a check shows the calibration has drifted beyond the permitted tolerance, the work performed since the last valid check is re-examined. Calibration times and results form part of the inspection record.
Step-by-Step Ultrasonic Testing Procedure
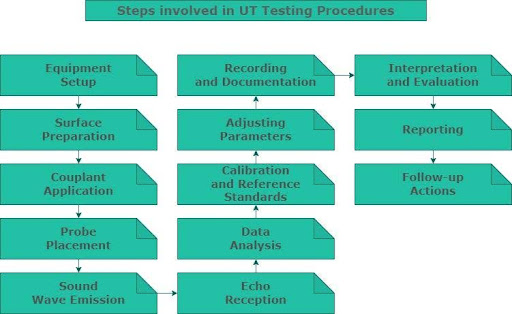
Steps Involved in UT Testing Procedure
1. Review the Procedure and Acceptance Criteria:
Confirm the governing procedure, the technique specified, and the acceptance criteria that apply before any equipment is set up.
2. Equipment Setup:
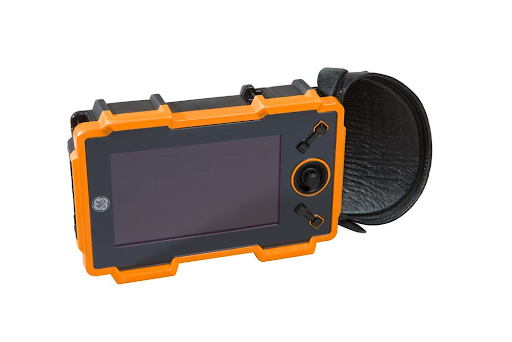
Assemble the ultrasonic testing equipment, including the flaw detector, the appropriate transducer and wedge, and confirm the instrument checks are current.
3. Surface Preparation:
Clean the material's surface, ensuring it is smooth and free from contaminants that could interfere with sound transmission.
4. Calibration:
Calibrate the sweep range and set the reference sensitivity on the appropriate calibration block, establishing DAC or TCG as required, and apply any transfer correction. Record the calibration.
5. Couplant Application:
Apply a suitable couplant between the transducer and the surface for efficient sound transmission, using the same couplant used during calibration.
6. Probe Placement and Scanning:
Position the transducer on the material's surface and scan to the pattern, overlap and speed defined in the procedure, maintaining consistent coupling and ensuring the required coverage is achieved.
7. Sound Wave Emission:
Ultrasonic waves are emitted into the material through the transducer, propagating until they encounter a boundary or a discontinuity.
8. Echo Reception:
The transducer receives echoes generated when ultrasonic waves encounter boundaries or discontinuities within the material.
9. Data Analysis:
Analyse the time of flight and amplitude of echoes to determine the location and size of indications, and assess whether they are relevant or geometric.
10. Adjusting Parameters:
Optimise instrument settings within the limits the procedure permits, recognising that changes to essential variables may require the procedure to be requalified.
11. Calibration Check:
Verify the calibration at the required intervals and at the end of the examination, and re-examine the relevant area if it has drifted beyond tolerance.
12. Interpretation and Evaluation:
Interpret the data and evaluate recorded indications against the acceptance criteria of the governing code.
13. Recording and Documentation:
Record inspection results and the supporting data, including equipment and probe identification, calibration details and technique parameters.
14. Reporting:
Generate a detailed report summarising inspection findings, including indication location, length, depth and evaluation, together with the personnel qualification and any limitations on coverage.
15. Follow-up Actions:
Based on inspection results, take appropriate follow-up actions such as repair, further testing or monitoring.
Adhering to a standardised procedure is essential to ensure the accuracy and reliability of the inspection process.
Ultrasonic Testing Procedures- An Enabler of Longevity
Performing ultrasonic testing is a carefully controlled process that relies on capable equipment, correct technique, and the judgement of qualified personnel.
From equipment setup and calibration through to the interpretation of results, each step contributes to a result that can be relied on and defended.
As a core method within non-destructive testing, ultrasonic examination reflects the precision and rigour of the discipline, and contributes directly to the integrity and service life of structures and materials across industry.
Key Takeaways
- Ultrasonic testing is a non-destructive method that uses high-frequency sound waves to detect internal discontinuities without damaging the component.
- The process involves transmitting ultrasonic waves into the material, receiving echoes, and analysing time of flight and amplitude to detect and characterise discontinuities such as cracks, voids, laminations and wall loss.
- The technique must suit the discontinuity: straight beam for laminations and thickness, angle beam for welds, TOFD and PAUT for detection and sizing on critical work.
- Calibration determines the validity of the result. Sweep range, reference sensitivity, DAC or TCG, transfer correction and interval calibration checks all belong in the procedure and the record.
- Screen height linearity and amplitude control linearity are periodic instrument verifications of amplitude response, not measures of depth accuracy.
- Ultrasonic testing is not universal — attenuative materials such as coarse-grained castings and austenitic welds, and discontinuities oriented parallel to the beam, remain difficult.
- Where the referencing code requires procedure qualification, changing an essential variable requires the procedure to be requalified by demonstration.
FAQs
1. Why is a well-defined Ultrasonic Testing procedure important?
A: A well-defined procedure ensures consistency, safety and quality assurance by providing clear guidelines and minimising errors. It also makes the examination defensible, since a reviewer can trace how the result was obtained — which technique, which calibration, which acceptance criteria.
2. What are the key components of an Ultrasonic Testing procedure?
A: Scope, references, general requirements, the inspection procedure itself, evaluation of indications, acceptance criteria, and documentation and reporting formats.
3. How is an ultrasonic testing system calibrated?
A: The sweep range is calibrated against known reflectors on a standard block such as the IIW V1 or V2 so that displayed distance corresponds to sound path or depth. Reference sensitivity is then set on a calibration block containing reflectors of known size at known depths, with a DAC curve or TCG applied to compensate for signal loss with distance, and a transfer correction where the component's surface or attenuation differs from the block. Calibration is rechecked at defined intervals and at the end of the examination.
4. What is the difference between an indication, a discontinuity and a defect?
A: An indication is the signal displayed by the instrument. A discontinuity is the physical feature producing it, once the indication has been shown to be relevant rather than geometric. A defect is a discontinuity that exceeds the acceptance criteria of the governing code and therefore requires repair or rejection.
5. What limits ultrasonic testing?
A: Attenuative materials such as coarse-grained castings and austenitic stainless steel welds scatter the beam; discontinuities lying parallel to the beam reflect little energy back; thin sections and the near-surface region are complicated by the initial pulse and near field; and results depend heavily on the skill of the operator. Complex geometry may also prevent adequate coupling or coverage.


There are no comments yet!