Abstract
As MEWP’s lift humans up to as much as 110 metres, the need for monitoring the structural integrity of this type of equipment to ensure safe operation is critical. Within the regulations of South Africa, which include the Occupational Health and Safety Act and the South African National Standards there is no requirement that any form of NDT is to be carried out in order to ensure the structural integrity of these types of equipment. This paper looks at the implementation of a complete NDT program using acoustic emission, ultrasonic, magnetic particle, dye penetrant and visual inspection methods. It will highlight specific case studies where the current inspection requirements failed to detect major defects. A complete NDT inspection program will help to ensure that the owners of these types of equipment have in fact taken preventative action to ensure operator safety regardless of the short comings of regulatory requirements.
1. Introduction
The focus of this presentation is to enlighten and educate. I will voice my opinion on certain aspects of the Lifting Machine Inspection industry in South Africa but also supply factual data. I will use my experience in N.D.T and A.E Load testing of M.E.W.P’s to give the reader a better understanding of the benefits and limitations of N.D.T, and with regards to A.E explain why data analysis in this method is so important and why experience is essential in correctly assessing a lifting machine.
2. Past practice
As a Lifting Machine Inspector, there are times when you walk away from a lifting machine and have a sense of doubt, did you find anything you were not sure of, did you find all the defects? Did you miss something? The implications of answering yes to any of those questions has the possibility of being severe, mostly to the person operating the machine or anyone in near proximity to it when it fails. In the event of such a failure very little responsibility falls on the inspector, simply because the inspection that was done reflects the condition of the truck at the time of the inspection and the inspector cannot control what happens to the machine once it leaves his sight, and let’s face it not everyone out there operating these machines use them solely for their intended purpose. So it goes without saying that as lifting machine inspectors we “should” use every available technique to find every possible defect at the time of the inspection as this is our only opportunity to make sure it’s as safe as it can be when it leaves. This is a very real concern when you as an inspector are only armed with your naked eyes, a load cell and maybe some form of micrometer to measure deflection. How can the probability of detection be increased, how can we inspect a machine and walk away from it with confidence, knowing that we have done everything in our power and used everything at our disposal to ensure the safety of these machines? N.D.T and a complete inspection program is a good way to start.
3. Proposed new practice.
The Comprehensiveness of lifting machine inspections is a highly debated subject and opinions on adequate methods to use when inspecting lifting machines vary from person to person. The main influence of these opinions, is exposure to N.D.T or a lack there of. The general perception seems to be that a standard overload test accompanied by a visual examination of the lifting machine is adequate to assess its structural integrity, however any person that has been exposed to and practised NDT methods will readily object to this being accurate. Lifting machine inspectors that do not incorporate NDT into their inspections are confident that the way they conduct an inspection is in their opinion sufficient to correctly assess a lifting machines condition, this is mainly due to a lack of information and by no means a fault of their own. It’s my opinion that a gap has formed in awareness, between L.M.I inspectors and the importance of N.D.T in their inspections.
It is not clear where this gap in awareness has stemmed from or if it has always been there but it is essential to the safety of lifting machine operators to close that gap as soon as practically possible. At present critical defects that are at the beginning stages of development are unintentionally being overlooked by lifting machine inspectors untrained in N.D.T and these machines are being put back into service. We are by no means saying that these units will fail in service, but it would be naive to assume the chances of failure have not increased significantly because of this error. A Complete Lifting Machine inspection program must be adopted as a norm, It should basically be an “enhanced” version of a standard L.M.I inspection. By “enhanced” we mean in addition to the standard visual inspection, N.D.T methods should be applied to critical areas of concern and the way to identify these critical areas is to utilize A.E monitoring whilst performing a Standard Load test. The A.E monitoring allows us to identify potential problem areas on a lifting machines structure that otherwise would have gone unnoticed, and then direct the more conventional N.D.T methods to those areas. A.E then, is used as a location or assessment tool and the more conventional N.D.T is used to accept or reject any discontinuities found in those areas. Apart from accepting or rejecting discontinuities found during the visual inspection of the Lifting machine, conventional N.D.T works in conjunction with A.E to locate defects that would have gone unnoticed and potentially resulted in the failure of a machine.
4. Case studies
N.D.T allows us to identify defects that could possibly have been overlooked by a normal visual inspection, defects that are not visible to the naked eye and that are in the beginning stages of damage. It allows us to pinpoint them and have them repaired before they fail and when you correctly combine these N.D.T methods it becomes a powerful tool in the inspection of a lifting machine and I believe is the only way to determine its true condition.
Below are few examples of defects in critical areas of lifting machines. If these components were to fail, the machine would almost definitely experience freefall and catastrophic failure, the point is that these defects are not visible to the naked eye but were located using N.D T methods.


It is impossible to see into solids like booms and welds, so performing a visual inspection on a boom, structural weld or attachment pin is not sufficient to determine its condition. These are examples of defects found in the initial visual inspection before any operation or load testing is performed, depending on the severity of the defect the operation and load test of the machine might have to be aborted until those initial defects are repaired. There is a specific order in which the inspections should take place, the lifting machine is first visually inspected and any suspect or critical areas are investigated further using the various N.D.T methods. Once the lifting machine is found to be safe to operate, a full operational inspection is performed and any suspect movements or sounds are investigated visually and if needed using N.D.T. Once the operational inspection is performed and the inspector is happy with the condition, a monitored load test is then performed using A.E sensors that are placed throughout the lifting machine’s structure. The A.E is used as a location and assessment tool, by capturing data from the sensors pinpointing problem areas and directing the inspector to those areas, for further investigation with more conventional N.D.T methods.
Why incorporate Acoustic Emission into the load test.
Although using conventional N.D.T methods could make finding flaws easier, the possibility remains that internal flaws could be hidden and the possibility for human error still exists in visual inspection. A.E gives us the extra tool we need to detect these kinds of hidden flaws, but the correct interpretation of data is essential. Utilizing A.E it becomes possible to locate and pinpoint structural defects in the metal as well as the fibreglass components and can also indicate hydraulic problems in cylinders and locking valve
Example of defect found in a fibreglass boom utilizing Acoustic Emission.

You will notice in the above graph that the activity recorded in the A.E load test was unusually high on channels 2 and 3 these sensors were attached to the fibreglass section of the upper boom.

In the above graph you will notice that although there was a clear reduction in activity between the first and second load cycles as per Pass/Fail criteria, there was excessive activity in the holding periods of the load test and activity actually increases towards the end of the holding period which is unacceptable, there should be no activity after the first minute of the holding period or at least a clear reduction in activity. The high activity was of concern and the boom was lowered to repeat the visual inspection in the area of concern and followed up with other N.D.T techniques as required.

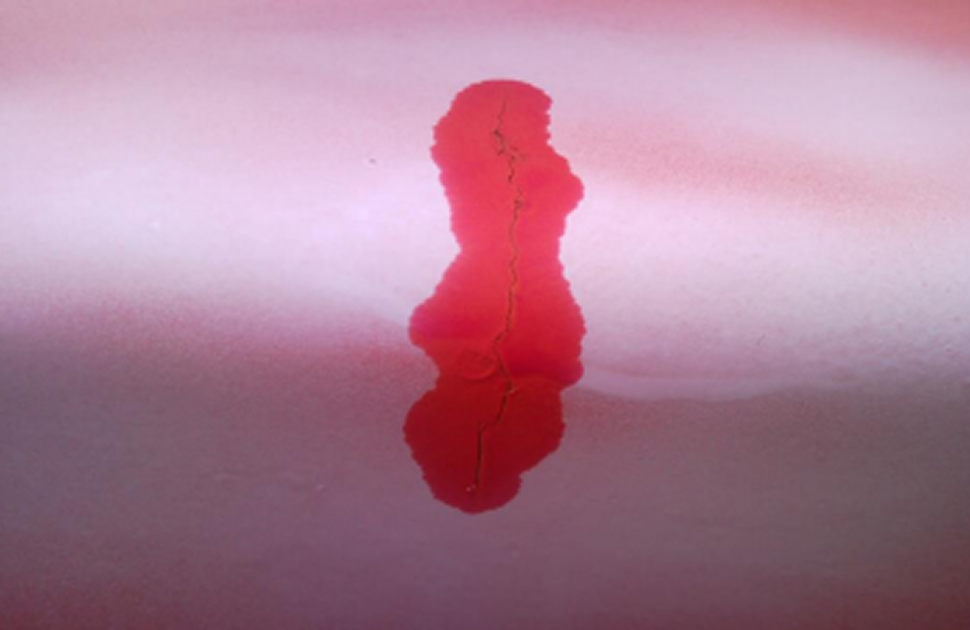
On closer inspection I noticed some fine horizontal cracks in the Non-conductive gel coating of the boom, possibly only surface paint cracking, but a Dye penetrant inspection was performed and revealed continues bleed out.
I relayed the findings onto the client, indicating that I believed the boom to be cracked. Below is a Photo of the bleed out from the dye penetrant inspection. Bare in mind, it is a close-up shot of the crack and was not visually blatant on the initial visual inspection.

The client wanted to confirm the findings and was willing to investigate further destructively. The client used a pencil grinder and grinded into the cracked area that I had identified. Above is a photo of the depth that was grinded too and a clear indication of a crack running into the boom remained.
It is important to note that without the Acoustic Emission data alerting me to the potential problem and without the follow-up dye penetrant inspection, this defect would have gone unnoticed and the unit would have been placed back into service with the defect remaining.
Example of defect found in metal utilizing Acoustic Emission.
Unlike the previous example, in this inspection relevant A.E data was overlooked by a inexperienced Inspector from a different company and the subsequent result was catastrophic failure of the upper boom’s metal section.
The unit in question underwent an A.E load test, the data captured during this test shows irregularities in both the Fiber boom and in the metal section of the upper boom at the elbow area (see figures 1 & 2 - Channels 2 & 3)
Fig 1

Fig 2

The amount of Hits recorded on the Fiber Boom (35938) on channel 2 is unacceptable, the amount of high threshold hits (320) Low duration hits(329) and counts (982715) recorded on channel 3 (Metal section) is unacceptable. (Figure 3) shows constant activity throughout the holding periods were there should be no activity or at least a reduction in activity, the activity also increases when the unit is being unloaded. All of this is unacceptable and indicates movement or propagation in the metal.

The unit was failed and sent for repairs, but only with the fiber boom being identified as defective. According to maintenance records the unit had the fiber boom replaced and was returned around 3 months later. An A.E load test was then performed again, the result of which was, no irregular activity was noted. This was correct, there was no relevant data emitted from the metal section of the upper boom that previously emitted unacceptable data, no relevant data was emitted from the fiber boom. The reason for the lack of relevant data in the metal is, unlike fiber that will seat, or settle back to its original position after a period of time, weakened or damaged metal will not. The damaged section had already been stressed to a point and crack propagation had already reached its maximum length at the previous load test done, so a lack of activity in the Load test done after the repairs would be expected.
It’s my opinion that the damage that caused the failure to occur had happened prior to the first acoustic emission load test being done and prior to the replacement of the fiber boom. The primary A.E result is the first test done before the repairs. The metal section should also have been ear marked as a primary concern according to the results from that test.
Conclusion
I believe that the majority of Lifting Machine Inspections being performed currently are superficial and lack essential aspects to ensure sufficient defect delectability. A complete inspection program combining A.E inspection with load testing and other N.D.T methods is vital to correctly determining the condition of a lifting truck. I believe a complete inspection program needs to be adopted throughout the lifting industry and current L.M.I’s need to be educated to the advantages of N.D.T and how it can increase the probability of defect detection, not only ensuring safer units in the field but also peace of mind for the inspector.