
Table Of Contents
- Introduction
- How Ultrasonic Testing Works
- Advantages of Ultrasonic Testing
- Disadvantages of Ultrasonic Testing
- Practical Applications and ROI Examples
- Conclusion
Introduction
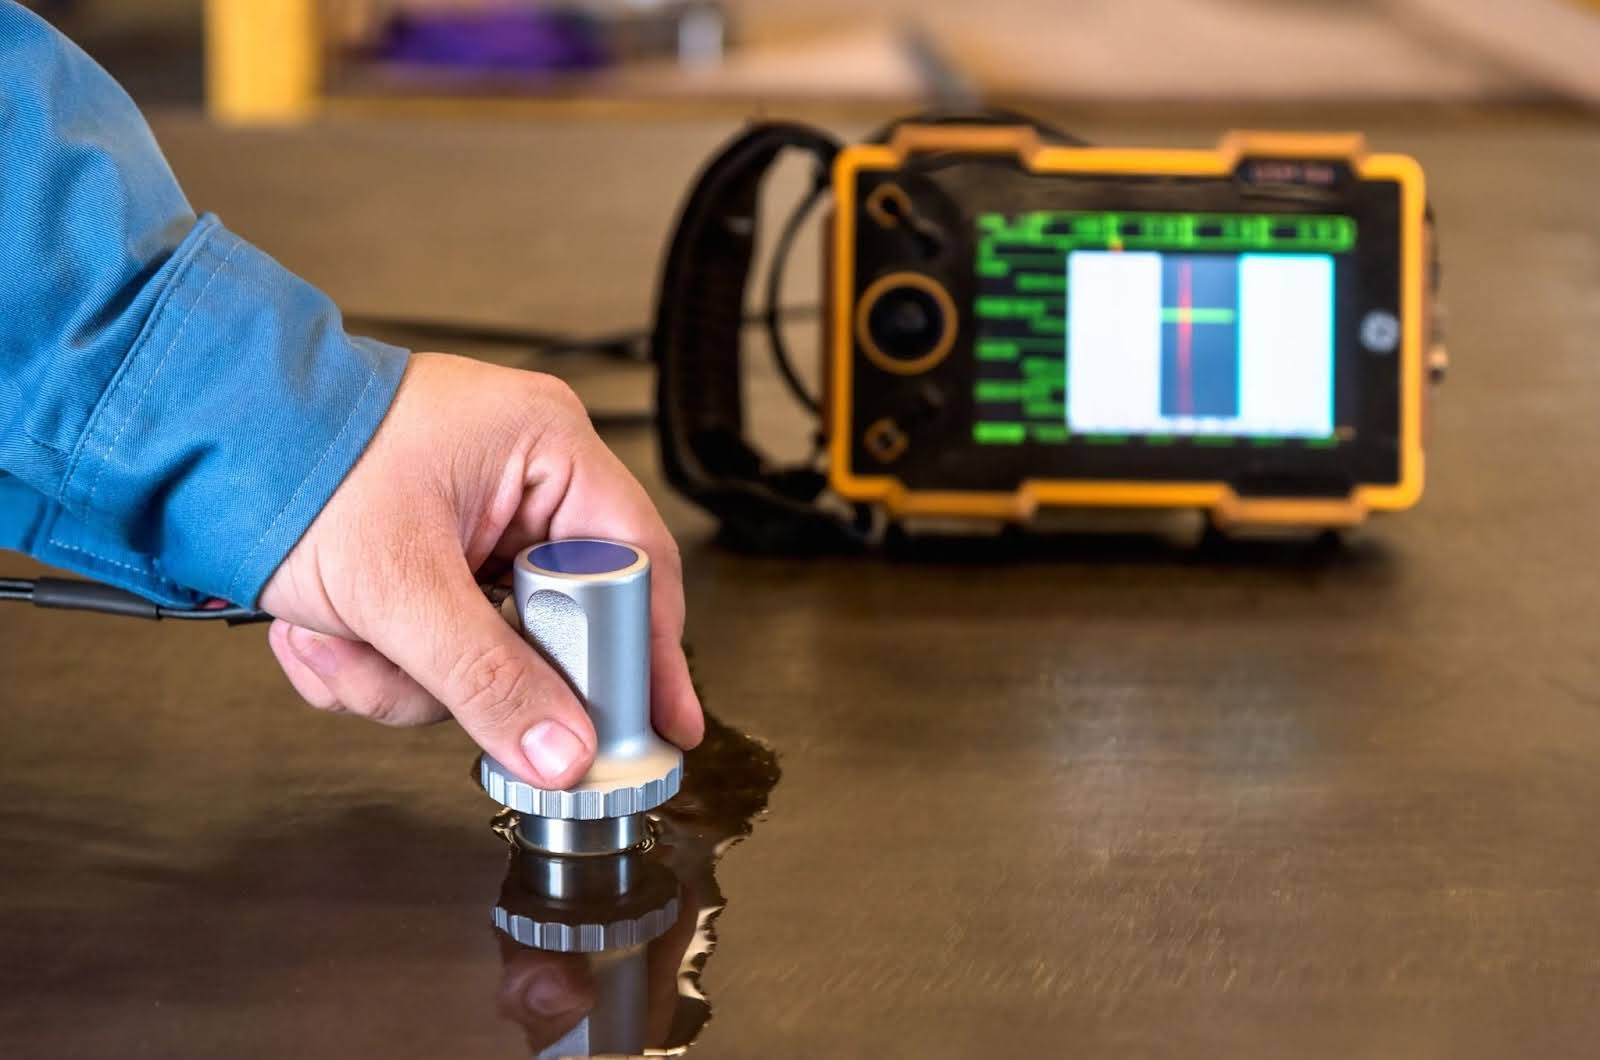
Imagine an engineer standing beside a large steel pipeline in a remote oil field. The stakes are high: a single undetected crack could lead to a multimillion-dollar failure. Yet she does not cut into the pipe or take it apart. She picks up a small portable instrument, presses a probe to the surface, and sends a pulse of sound into the steel. Within moments, she knows what lies beneath the surface. That is the capability of ultrasonic testing (UT).
UT is a fundamental tool in modern industry, used to examine welds, forgings, castings and complex aerospace components without leaving a mark on them. It uses high-frequency sound waves to look deep inside materials and reveal internal defects. From oil and gas pipelines to aircraft wings, UT plays a central role in maintaining structural integrity and safety.
Non-destructive testing (NDT) professionals, engineering students and industrial researchers are regularly faced with choosing the right inspection method for a given job. Understanding the benefits and drawbacks of ultrasonic testing — its accuracy, safety, real-time capability and limitations — is essential to making that choice well.
This article sets out how UT works, its main advantages and disadvantages, and how those play out in practice. Whether you are considering phased array ultrasonic testing (PAUT) or comparing inspection techniques for critical infrastructure, it is intended as a practical basis for deciding when UT is the right method and when it is not.
How Ultrasonic Testing Works
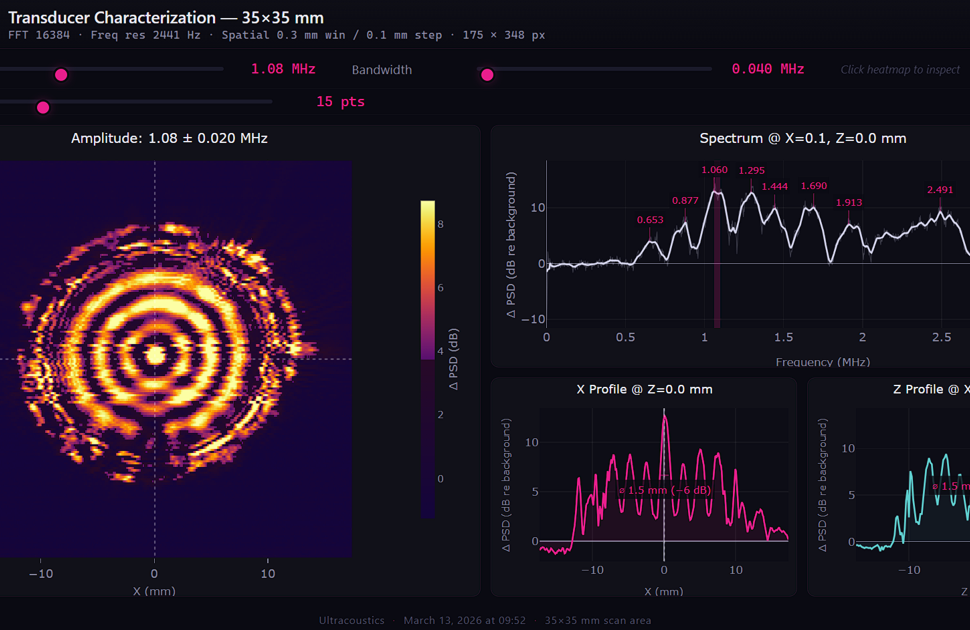
Ultrasonic testing uses high-frequency sound waves, typically between 0.5 and 20 MHz, to detect internal flaws in materials. A transducer introduces ultrasonic pulses into the material. When the sound meets a discontinuity such as a crack or void, part of the energy is reflected back to the transducer. The time of flight and amplitude of these reflections are analyzed to determine the location of the flaw and to estimate its size and nature.
Common UT techniques include pulse-echo, through-transmission, time-of-flight diffraction (TOFD) and phased array ultrasonic testing (PAUT). The process involves calibrating the equipment, applying a couplant — such as gel or water — to transmit sound between probe and part, and then scanning the test surface. Measurement accuracy and real-time results are what make UT a preferred method for many NDT professionals.
Advantages of Ultrasonic Testing
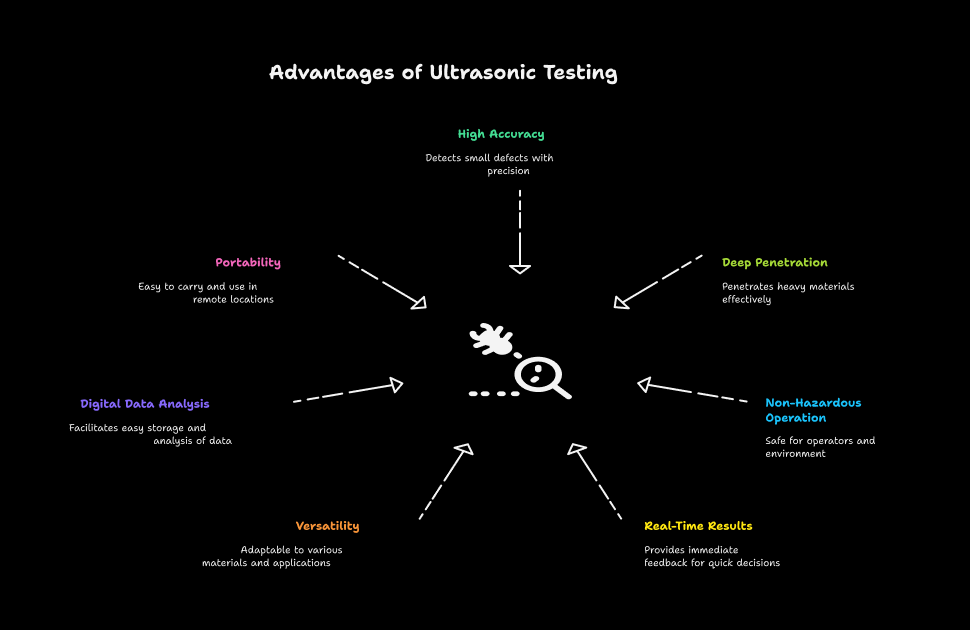
1. High Accuracy and Sensitivity
UT is highly sensitive to small internal defects such as cracks, inclusions and voids. The smallest detectable flaw depends on the frequency used, the material, and the size, shape and orientation of the flaw relative to the beam. In weld inspection, UT is used to determine the size, depth and orientation of defects, which directly informs repair decisions. Advanced techniques such as PAUT use a multi-element probe to steer and focus the beam electronically across a range of angles, improving defect evaluation in complex geometries such as pipeline girth welds.
2. Deep Penetration
UT can penetrate thick sections — in fine-grained steel, several meters in favorable conditions. This makes it well suited to heavy components such as pressure vessels and large forgings, where methods such as radiography become impractical. By selecting the frequency, the inspector balances penetration against resolution, which allows reliable results across a wide range of material thicknesses.
3. Non-Hazardous Operation
Unlike radiographic testing, which uses ionizing radiation, UT uses sound waves that pose no radiation risk to the operator or nearby personnel. There is no need for exclusion zones, shielding or radiation permits, which makes UT safer and more practical in operating facilities. The absence of radiation also reduces compliance costs and avoids the operational disruption of clearing work areas.
4. Real-Time Results
UT gives immediate feedback, with digital instruments displaying indications during scanning. Inspectors can make decisions on the spot, which shortens the overall inspection. In pipeline weld inspection, for example, real-time results allow defects to be identified and repaired promptly, reducing downtime during time-critical work.
5. Versatility Across Materials and Applications
UT works on a wide range of materials — metals, composites and ceramics — provided they transmit sound adequately. It is used in aerospace on composite laminates, in oil and gas on pipeline welds, and in power generation on turbine rotors, shafts and discs. Its adaptability is extended further by the choice of technique, such as immersion or contact UT, tailored to the component.
6. Analysis Digital Data
Modern UT instruments produce digital data that is easy to store, analyze and share. This supports predictive maintenance by allowing defect growth to be tracked over time. UT thickness measurement on pipelines, for example, can track corrosion rates so that maintenance is planned rather than reactive. Electronic records also simplify regulatory compliance and audits..
7. Portability
UT equipment, particularly handheld instruments, is compact and suited to field use. Portable systems allow inspections at remote sites such as offshore platforms and remote construction projects. Battery-powered units provide mobility and allow UT to be used in harsh conditions without loss of accuracy.
Disadvantages of Ultrasonic Testing
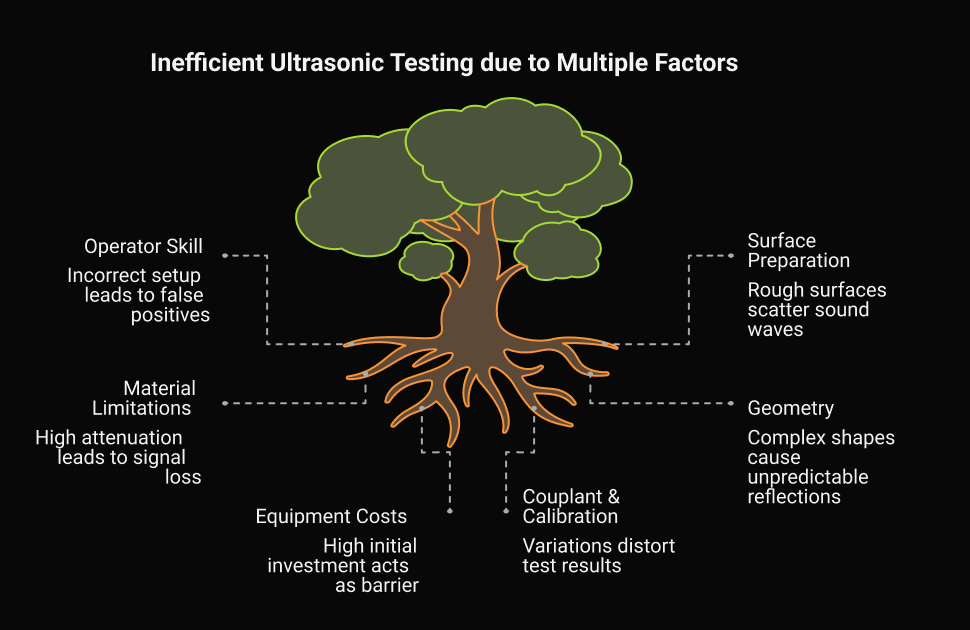
1. Operator Skill Dependency
UT depends heavily on the skill of the operator. Thorough training and certification — typically to Level II or Level III under a scheme such as ASNT SNT-TC-1A or ISO 9712 — is needed to calibrate correctly, select probes and interpret signals. Incorrect setup or misinterpretation can result in false calls or missed defects. A complex weld, for example, can produce multiple geometric reflections, and only a skilled interpreter can reliably distinguish a genuine flaw from background noise.
2. Surface Preparation Requirement
UT requires a clean, reasonably smooth surface for sound to enter the material effectively. Rust, scale and rough surfaces scatter the sound and reduce accuracy. A couplant must also be applied to exclude air between probe and surface, which adds a step to the preparation. On large field assets such as pipelines, cleaning is time-consuming and labor-intensive, which increases inspection cost.
3. Lack of Performance on some Substances
UT performs poorly in materials with high sound attenuation, such as coarse-grained castings and porous composites. In these materials the sound is scattered or absorbed, reducing signal clarity. Welds in austenitic stainless steel are a well-known example: their coarse, directional grain structure scatters and deflects the beam, and often requires specialized probes or techniques.
4. Geometry Limitations
Complex shapes, such as curved surfaces or irregular weld profiles, can complicate UT inspection. Sound may reflect unpredictably, producing spurious indications or masking real defects. PAUT addresses this with multi-angle beam steering, but it requires more sophisticated equipment and expertise, which adds cost. Conventional UT is often unable to inspect highly complex parts such as turbine blades reliably.
5. Equipment Costs
UT is economical over the long term compared with radiography, but the initial cost of equipment is significant, particularly for advanced systems such as PAUT. High-frequency transducers, digital flaw detectors and software licences all contribute. For smaller operations this upfront expense can be a barrier, although long-term savings often justify the investment.
6. Couplant and Calibration Sensitivity
UT accuracy depends on consistent couplant application and accurate calibration. Variations in couplant thickness or lapses in calibration can distort results. In contact UT, for example, poor coupling weakens the signal and can cause defects to be missed. Regular calibration checks are required, which adds to the process.
7. Impaired Visual Output
Unlike radiographic testing, UT relies on signal interpretation rather than a direct visual image of the part. Its output is less intuitive than a radiograph and harder to communicate to non-specialists. PAUT can produce two- and three-dimensional images, but these are more complex and require specialized software and training to interpret.
Practical Applications and ROI Examples
UT's combination of strengths makes it one of the most widely applied NDT methods, and its value shows most clearly in practice. In oil and gas, UT inspection of pipeline girth welds allows cracks to be found early, avoiding the far higher cost of repairing a failure in service. Its real-time results and portability also shorten inspection time, which reduces costly downtime. In aerospace, UT detects delaminations in composite structures, preventing unscheduled in-service failures and the costs that come with them.
Its limitations appear just as clearly. On coarse-grained castings, signal noise can make UT results inconclusive, requiring further testing. In cases like these, combining UT with another method provides a complete inspection.
1. Optimal Ultrasonic Testing
To get the full benefit of UT, organizations need to invest in training so that signals are interpreted accurately, and to apply advanced techniques such as PAUT to complex geometries. Proper surface preparation and calibration are essential for valid results. Where materials or shapes are difficult, limitations can be overcome by combining UT with a complementary method such as radiographic testing. Digitalization and AI-assisted analysis can further improve accuracy by reducing operator error and identifying defect trends that support predictive maintenance.
2. Getting the Right Method
Knowing the strengths and weaknesses of UT is essential for NDT professionals, students and researchers building a sound inspection plan. Its accuracy, penetration, safety and versatility make it suitable for a wide range of weld and material inspections. Its dependence on operator skill, its surface preparation requirements, and its limitations with certain materials and geometries must also be considered. With appropriate training, equipment and procedures, UT delivers dependable results. If you are unsure whether UT is the right choice for your project, a detailed method-selection review with qualified NDT service providers can help identify the safest, most efficient and most cost-effective approach.
Conclusion
Ultrasonic testing is a highly capable NDT method that offers good accuracy, operator safety and real-time results for the inspection of welds and materials. It penetrates thick sections and produces digital data of real value in oil and gas, aerospace and manufacturing. It also depends on skilled operators, requires surface preparation, and is limited on certain materials and geometries. Applied with the right procedures and, where needed, advanced techniques, UT saves time and cost and helps prevent failures. Equipment and probes for UT can be compared through NDT products.
There are no comments yet!