

Table of Content
- Introduction
- What is Visual Inspection?
- Inspector Visual Requirements
- Step-by-step Procedure of the Visual Inspection of Welds
- Weld Preparation Techniques
- Visual Inspection in the Future
- Key Takeaways
- FAQs
- Sources
Introduction
Visual inspection after welding is very useful in evaluating quality, even where other testing methods are also to be employed. Surface flaws such as cracks, porosity and unfilled craters can be detected by visual inspection alone, leading to repair or rejection of the work. Welds must be cleaned of slag before the surface can be examined properly. A 10x magnifying glass helps detect fine cracks and other discontinuities, and borescopes and dental mirrors are useful for inspection inside vessels, pipes or confined areas.
It is worth being clear at the outset about what visual inspection can and cannot do. It examines the surface. Discontinuities below the surface — internal porosity, buried slag, incomplete penetration that is not visible from either side, internal lack of fusion — require volumetric methods such as radiographic or ultrasonic testing, and surface-breaking discontinuities too fine to see may need magnetic particle or liquid penetrant testing. Visual inspection is normally the first method applied and often determines which further methods are needed.
What is Visual Inspection?
Visual Inspection is the most popular and widely used of the non-destructive inspection techniques. Completed welds should be checked against the drawings and the specification. The most common welds that need to be inspected in the field are fillet welds. Fillet welds are designed on their leg sizes. If a leg is under the specified dimension, the joint has less strength than it was designed for. The throat of the weld should be checked as well.
Codes define the conditions under which visual examination is carried out, rather than leaving them to the inspector's judgement. ASME Boiler and Pressure Vessel Code Section V, Article 9 sets requirements for direct and remote visual examination, including the maximum eye-to-surface distance, the minimum viewing angle and the minimum illumination at the surface being examined, and requires that the examination be performed to a written procedure. For structural steel, AWS D1.1 sets out the visual inspection acceptance criteria and the conditions of examination. AWS B1.11, the guide for the visual examination of welds, is a useful practical reference. Internationally, ISO 17637 covers visual testing of fusion-welded joints.
Which document applies is determined by the contract, the specification or the governing code — not by preference. The same discontinuity can be acceptable under one code and rejectable under another.
Also read : The Significance of Visual Inspection in NDT
Inspector Visual Requirements
Performed with or without corrective lenses, the inspector must demonstrate near vision acuity on Jaeger J2 at not less than 12 inches, together with a colour perception test. These checks are normally required annually, and the records form part of the evidence an auditor will ask to see.
Vision acuity is one element of a wider qualification requirement. Personnel are qualified and certified under a recognized scheme: an employer's written practice based on ASNT SNT-TC-1A (currently at its 2024 edition) or ANSI/ASNT CP-189, or third-party certification under ISO 9712:2021. In welding fabrication, the AWS Certified Welding Inspector (CWI) qualification under AWS QC1 is widely specified. The distinction matters in practice — under SNT-TC-1A the employer is the certifying authority and the certification is not portable, while ISO 9712 certification is issued independently and travels with the individual.
The objective of visual inspection is not only to detect non-permissible discontinuities but to verify all the procedural details. If the drawing shows a fillet weld at 5/16 inches, then each leg of the weld needs to measure to that dimension.
A fillet weld gauge is the standard tool for checking weld sizes. It has two corners for checking leg sizes and two corners for checking the throat of the weld. An explanation of how to use the fillet weld gauge is shown below:
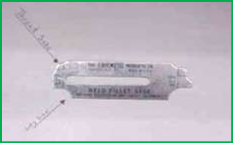
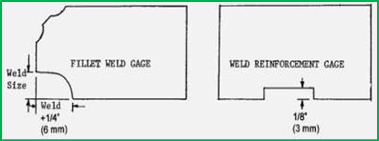
The initial procedures taken by the Welding Inspector are:
a. Details to Check Before the Welding:
- The materials to be welded and the related standards (ASME, ASTM)
- Welder qualification certificate, drawings, and related documents
- Welding equipment and electrodes, including storage and drying systems
- The welding procedure specification (WPS) and its approval status
- Welding edge preparations and correct bevels
- Root openings
- Clearance of backing strip or ring
- Overall alignment and fit-up
b. Details to Check During the Welding:
- Preheat and interpass temperature
- Cleaning, chipping, grinding or gouging between passes
- Compliance with the welding parameters of the WPS
- Structural defects and discontinuities as welding progresses
c. Details to Check After the Welding:
- Dimensional accuracy of the weldment, using fillet weld gauges or rulers, as shown above
- Conformity to drawing and procedure requirements
- Acceptability of welds with regard to appearance and fabrication quality
- The presence of any unfilled craters, undercut, cracks or overlap
- Arc strikes on the base metal
- Post-heat treatment temperature, when specified
d. Weld Joint Preparation:
The first step in making a sound weld is to make sure the joint is correctly cleaned, using a stiff wire brush or a grinder to clean the base metals. The portion of the base metal to which the ground clamp will be attached must also be cleaned. Poor contact at the ground clamp creates resistance in the welding circuit and can result in poor weld quality.
Preheat before welding should be applied according to the procedure. All unpainted surfaces must be free from loose or thick scale, slag, rust, moisture, grease or other foreign material.
Step-by-step Procedure of the Visual Inspection of Welds
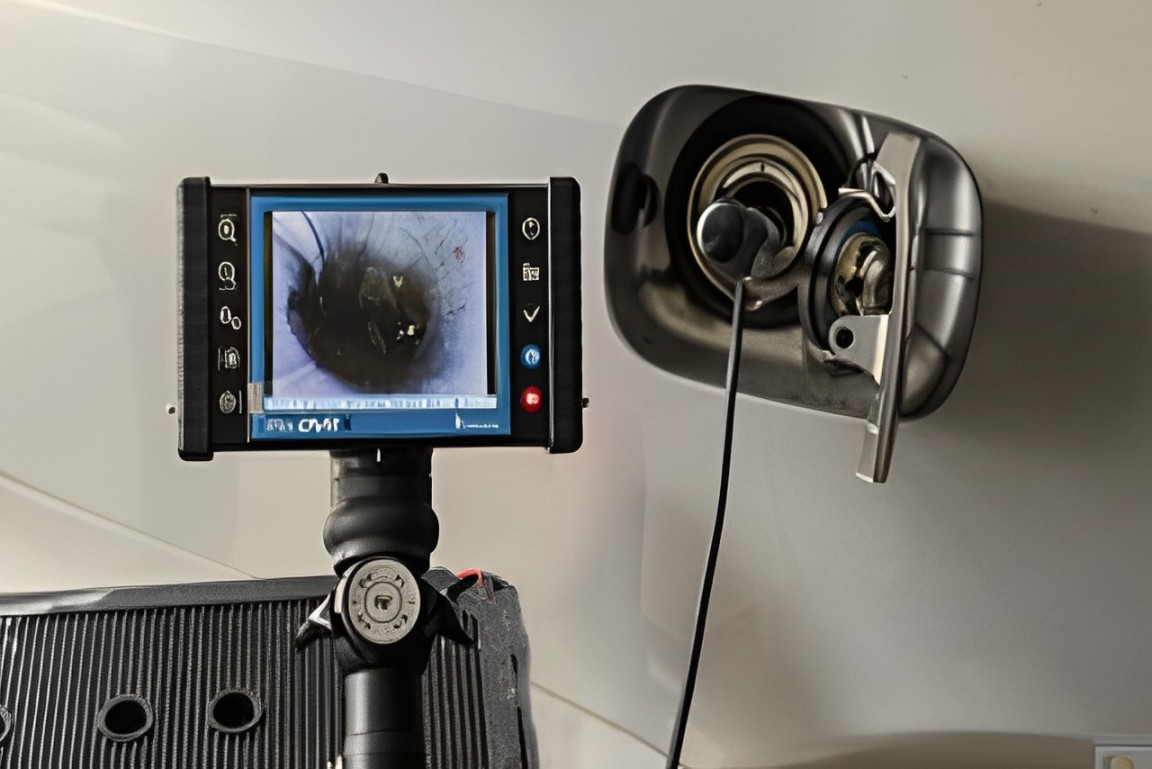
Visual inspection is a crucial method for evaluating weld quality. It is widely used because of its simplicity, low cost and ability to detect surface flaws. Its advantages include suitability for on-site assessment, immediate results and minimal equipment requirements. Visual inspection techniques vary with the application and include direct visual examination, remote visual inspection and video inspection.
1. Before Inspection
Gather the necessary tools, such as magnifying glasses, flashlights and inspection gauges. Ensure adequate lighting and access to the weld area. Review the welding specifications and standards applicable to the project, and confirm the acceptance criteria that apply to this weld and this connection type before starting.
2. During Inspection
Inspection Techniques:
- Direct Visual Examination: Observe welds directly using the naked eye or with the aid of magnification tools, within the distance, angle and illumination conditions set by the governing code.
- Remote Visual Inspection: Use cameras or borescopes to examine welds in confined or inaccessible areas. Where the result is to be used as code-compliant examination, the system must provide resolution at least equivalent to direct observation, and this is normally demonstrated with a resolution target before and after the examination.
- Video Inspection: Record video of welds for detailed analysis and documentation.
3. After Inspection
Defect Identification:
- Surface Flaws: Look for indications of cracks, porosity, incomplete penetration, undercut, overlap or other discontinuities.
- Weld Geometry: Check for proper weld size, shape and alignment according to specification.
- Joint Integrity: Verify the integrity of the weld joint and assess its suitability for the intended application.
Each indication is then evaluated against the acceptance criteria of the governing code. A discontinuity only becomes a defect when it exceeds those limits — cracks being the exception, as they are not permitted regardless of size under AWS D1.1 or the ASME construction codes.
- Record Inspection Findings: Document observations, measurements and any detected discontinuities.
- Compliance Reporting: Prepare reports detailing compliance with welding procedures and standards.
- Nonconformance Reporting: Identify and document any deviations from acceptance criteria and recommend corrective actions.
The report should identify the component, the governing procedure and acceptance criteria, the inspector and their qualification, the equipment or gauges used, and the result — so that a reviewer can trace the decision without reconstructing it. Where indications require volumetric examination, the visual report is also the trigger for that further testing.
Following these step-by-step procedures before, during and after inspection can help inspectors assess welds effectively, identify defects and maintain quality standards in welding processes.
Read More : Welding Procedure Specification
Weld Preparation Techniques
Proper weld preparation helps create clean, well-aligned surfaces, which are crucial for achieving strong and durable welds. Visual inspection plays a significant role in verifying the effectiveness of weld preparation techniques. Some preparation techniques to be carried out on welds before inspection include:
1. Cleaning:
Thoroughly clean the weld area to remove any debris, dirt, oil or contaminants that could obscure discontinuities during inspection. Use wire brushes, solvents or grinding tools as necessary. Slag and spatter in particular must be removed, since either can conceal a surface flaw or be mistaken for one.
2. Surface Smoothing:
Ensure that the welding surface is smooth and free of rough edges, burrs or irregularities that could interfere with the inspection process or mask defects. Take care that surface conditioning does not remove evidence of a discontinuity or alter the weld profile beyond what the procedure permits.
3. Surface Marking:
Mark the weld area with appropriate identification, such as reference points or inspection locations, to facilitate accurate inspection and documentation. Use marking materials that are permitted for the base material — low-halogen or low-sulphur markers are commonly required on stainless steels and nickel alloys.
4. Access Preparation:
Ensure proper access to the weld area for inspection. This may involve removing obstacles, adjusting lighting or using inspection tools such as borescopes for internal inspections.
5. Pre-Inspection Verification:
Conduct a preliminary visual inspection to assess the cleanliness, alignment and overall condition of the weld area before proceeding with formal inspection procedures.
These preparation techniques help ensure that the weld area is optimally prepared for inspection, allowing inspectors to accurately assess weld quality and detect any defects or discrepancies.
Visual Inspection in the Future
Visual inspection methods have evolved significantly, driven by technology, automation and AI. What was emerging when this article was first written is now in routine industrial use, and the questions have shifted from whether these tools work to how their results are qualified.
Developments shaping visual inspection include the following:
1. Automated Visual Inspection:
Integrates robotics, computer vision and AI for defect detection and analysis. Fixed and robot-mounted camera systems with controlled lighting are well established for repetitive, high-volume surface inspection in manufacturing. Their role in code-governed work depends on whether the written procedure permits automated evaluation and how detection performance has been demonstrated.
2. AI-Assisted Visual Inspection:
Uses AI algorithms to analyse images and video, supporting defect identification and decision-making, and feeding trend data into predictive maintenance programmes. Automated defect recognition on inspection imagery has matured considerably in recent years. The practical questions on qualified work are how the system's detection rate and false call rate were established, whether the procedure allows it, and who signs the report — responsibility for the interpretation still sits with the certified inspector.
3. Remote Visual Inspection (RVI):
Employs cameras, borescopes or robotic systems for inspection in inaccessible or hazardous areas. Drones with high-resolution cameras are now standard for external structures and, in collision-tolerant form, for tank, vessel and confined-space interiors, removing the need for scaffolding or entry permits in many cases.
4. Drone and Robot-Mounted NDT Payloads:
The more significant recent shift is from drones as camera platforms to drones carrying contact instrumentation. Ultrasonic thickness measurement payloads are now available for confined-space inspection drones, giving live A-scan spot readings on steel in tank interiors, ship hulls and locations at height, with a remotely operated couplant dispenser at the probe. Magnetic crawler robots serve the same purpose on accessible vertical surfaces, combining visual survey with thickness readings in one deployment. The access changes; the method and the qualification behind it do not.
5. Digital Inspection Records and Digital Twins:
Images, video and positional data captured during inspection can be located on a model of the asset rather than described in text, allowing findings to be compared against earlier inspections and linked to the maintenance record. This supports trending and gives auditors a traceable history.
Automation and AI improve inspection efficiency, reduce costs and improve consistency, leading to better productivity and quality control across industry.
Key Takeaways
- Visual inspection has evolved from manual assessment to techniques integrating imaging, robotics and AI, improving efficiency and consistency.
- Visual inspection examines the surface only. Subsurface discontinuities require volumetric methods such as radiographic or ultrasonic testing.
- The conditions of examination — distance, viewing angle, illumination and, for remote inspection, resolution — are set by the governing code, not by preference.
- A discontinuity becomes a defect only when it exceeds the acceptance criteria of the applicable code. Cracks are the exception and are never permitted.
- Inspector qualification and annual vision checks are requirements, and their records form part of the inspection evidence.
- Automation, AI and remote inspection are in routine use today, but responsibility for interpretation remains with the certified inspector.
- Industries including manufacturing, construction, oil and gas, power generation and transport rely on these methods to ensure product quality, structural integrity and compliance with standards.
FAQs
1. How has visual inspection evolved with time?
A: Visual inspection has advanced significantly with technology, automation and AI. From manual assessment, modern practice integrates imaging technology, robotics and AI algorithms for defect detection and analysis, and increasingly places findings within a digital record of the asset rather than in a standalone report.
2. What industries benefit from advanced visual inspection methods?
A: Manufacturing, construction, oil and gas, power generation, aerospace, marine and rail all rely on advanced visual inspection. These industries use automated inspection systems, AI-assisted analysis and remote inspection techniques to improve productivity and quality control.
3. What defects can visual inspection of welds detect?
A: Surface-breaking and visible discontinuities — cracks, surface porosity, undercut, overlap, unfilled craters, arc strikes, incorrect weld size or profile, misalignment, and lack of fusion or incomplete penetration where it is visible from an accessible surface. Internal discontinuities are not detectable visually and require radiographic or ultrasonic testing.
4. What tools are used for visual inspection of welds?
A: Fillet weld gauges, bridge cam (Cambridge) gauges, undercut gauges, hi-lo gauges for pipe alignment, rulers and calipers, a 10x magnifier, adequate lighting and a light meter where illumination is specified, plus mirrors, borescopes and videoscopes for restricted access.
5. When should visual inspection be carried out?
A: At three stages — before welding, to verify materials, fit-up, edge preparation and qualification records; during welding, to check preheat, interpass conditions and compliance with the procedure; and after welding, to assess the completed weld against the acceptance criteria. Problems found before welding starts are by far the cheapest to correct.
Sources
- Picryl
- AQC Inspection
- Ceyrek Muhendis


There are no comments yet!